// Docs
Controller check
Every controller reads G-code a little differently. The controller check is a short program for the post you chose that tries the things that differ, in the air: every move stays at Z+5 mm or above.
The arrow next to Export G-code → Check this post → Controller check (air run)… shows the steps and downloads the file.
Before running
- Take everything off the table. Set Z zero well clear of it, or raise it.
- No cutter, or a short one. A hand on the stop button, the feed override low.
The steps
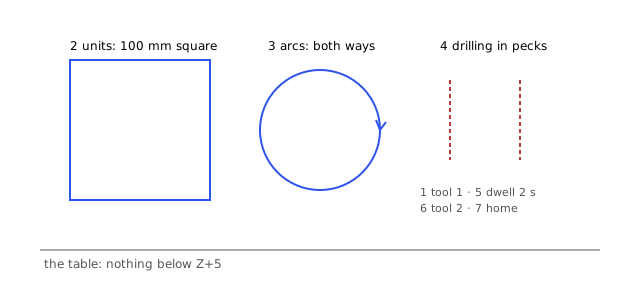
- Tool 1: the controller asks for (or changes to) tool 1, starts the spindle and waits about 3 s.
- Units: a 100 mm (4 in) square at Z+10. Measure it: not 25.4 times bigger or smaller.
- Arcs: a circle clockwise, then counter-clockwise.
- Drilling: two holes from Z+15 down to Z+5 in pecks.
- Dwell: the tool stops for 2 s.
- Tool 2: the spindle stops, the controller asks for tool 2, starts again.
- End: back to X0 Y0 at Z+25.
Each step is also written in the file, so the controller’s screen shows what should happen. If a step does something else, stop the machine and tell us which one.