// Docs
Heights and depths
Heights are measured from Z zero. With Z zero on the stock top (the default), cuts go below zero; with Z zero on the table, the stock top is at the stock thickness. The file says which (in its header).
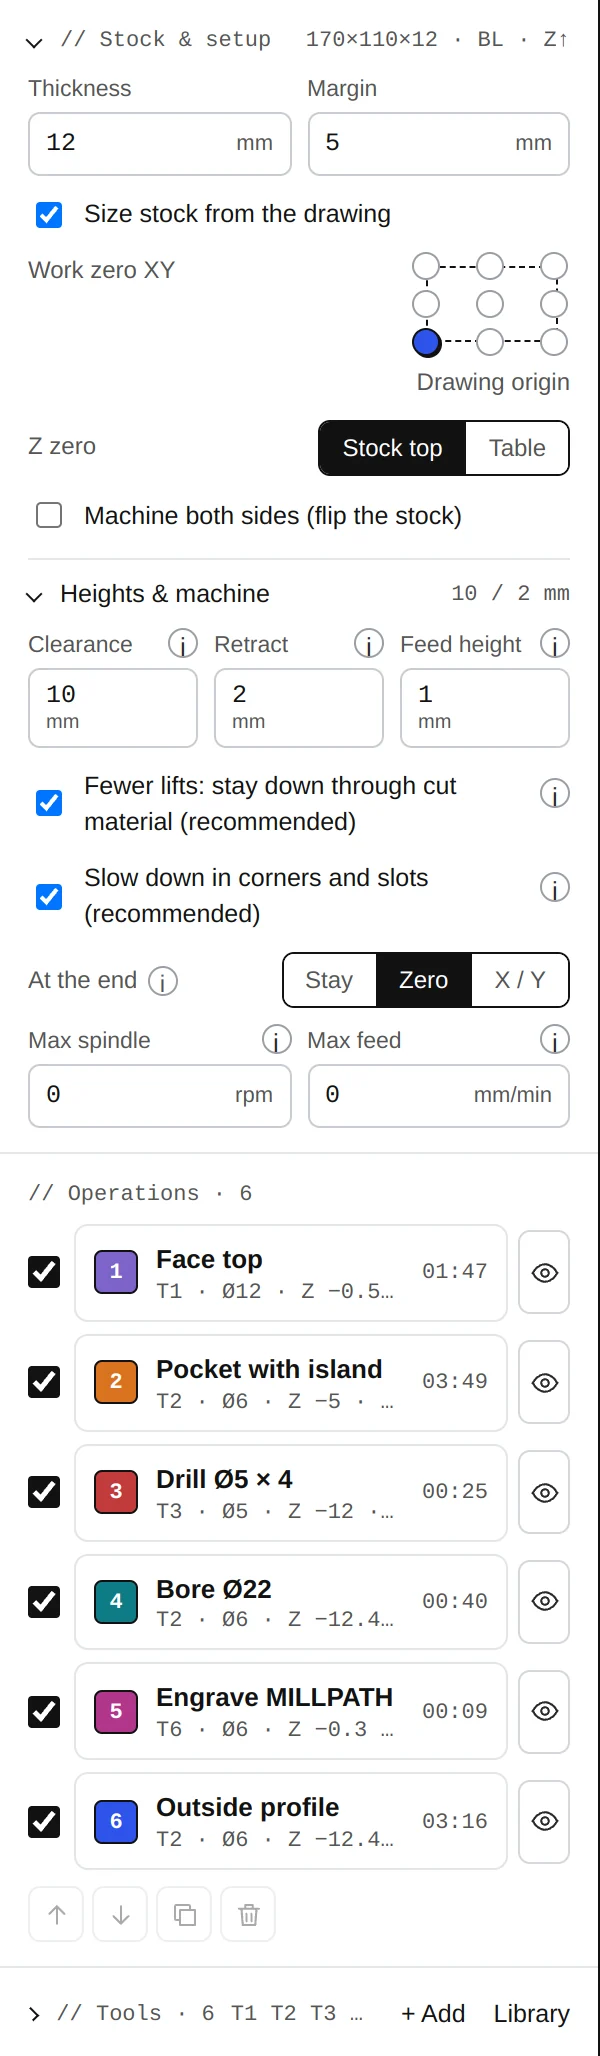
Both live at the top of the left panel. Stock & setup: thickness, margin round the drawing, size the stock from the drawing, the work zero, Z zero, and machining both sides. Heights & machine: clearance, retract, feed height, fewer lifts (stay down through material already cut), and below them the machine limits and where the tool waits at the end.
| Height | Used for |
|---|---|
| Clearance | Rapids between operations, at tool changes and at the start and end. Set it above clamps and vises. |
| Retract | Rapids between cuts of one operation, lower than clearance, so less time in the air. |
| Feed height | Rapid descents stop this far above the surface still to cut; the rest is fed, never rapid into material. |
| Start depth | (per operation) cutting begins this far below the stock top, when the material above is already gone. |
| Own safe heights | (per operation) its own clearance and retract, for example over a tall clamp next to one feature. |
Depths
Depth is how deep an operation cuts from the stock top. Stepdown splits it into passes. A cut-out profile goes a little below the stock (0.4 mm by default) so the part comes free; the safety checks flag any cut that goes below the stock bottom into the table.
At the end of the program the tool rises to clearance and waits where you choose under At the end: over the last cut, at the work zero, or at an X / Y.
Controller smoothing (LinuxCNC, Mach3 / Mach4 and Haas) lets the controller round the path a little so it keeps its speed through many short moves, as in 3D finishing. LinuxCNC gets G64 P with the tolerance you set, Haas G187 P3 E (and G187 at the end), Mach G64 (how much it rounds is set in Mach). 0 leaves it off, and the controller follows its own setting.
Clamps and keep-out areas
Under Stock & setup, Clamps and keep-out areas marks where clamps, vise jaws or screws stand: position, width, length and the height of their top above the stock top. They show hatched in 2D and as boxes in 3D. Rapids that would cross one rise to 2 mm above its top; a cut that reaches into one is flagged by the checks as Into a clamp.