// Operations · key P
Clears the area inside an outline to a depth, leaving islands where there are inner shapes.
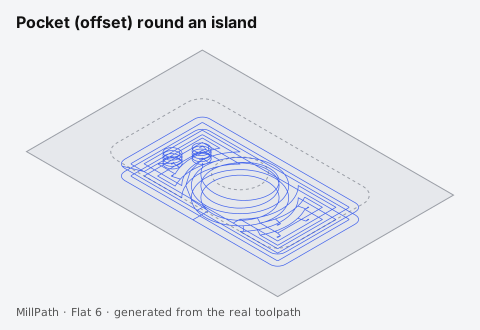
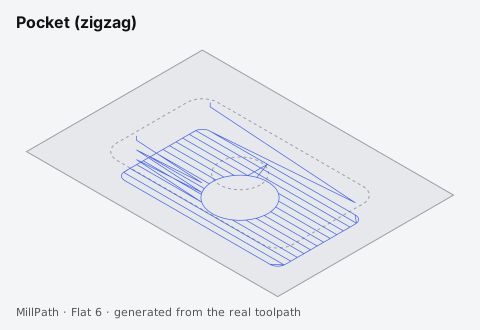
Use it for: Recesses, inlays, cavities, clearing around raised text or a logo.
Tool: A flat end mill; a smaller one for detail, a larger one for speed.
Settings
| Setting | What it does | Default |
|---|---|---|
| Depth | Depth of the pocket floor. | 5 mm (or the stock) |
| Stepdown | Stepdown. | 2 mm or the tool's own |
| Stepover | How far each pass moves sideways, as a % of the tool diameter. Lower is a smoother floor and slower. | 40 % |
| Pattern | Offset (rings, inside out), Spiral (one continuous spiral of constant step where the rings follow one another) or Zigzag at an angle (cut area by area, stepping along the wall between lines). | Offset |
| Direction | Climb or conventional. | Climb |
| Corners | Round (no relief), or dogbone / T-bone relief for inlays and square fits. | Round |
| Stock to leave | Left on walls and floor. | 0 |
| Finish pass on the walls | One last pass along the walls at full depth. | Off |
| Finish pass on the floor | The levels stop this much above the floor (0.3 mm by default), then the floor is cut in one last thin pass: a cleaner floor, and no level cuts the final floor twice. | Off |
Every operation also has: Tool, Include in G-code, Own safe heights, Start depth, Coolant, see Heights. Hover the (i) next to a setting in the app for the same explanations.
Tips
- Inner shapes become islands automatically: select the outline and the shapes inside it together.
- For large pockets with a big tool, follow with Rest machining using a smaller tool for the corners.