// Operations · key C
Profile
Cuts along an outline: around a part to cut it out, inside a hole, or on the line.
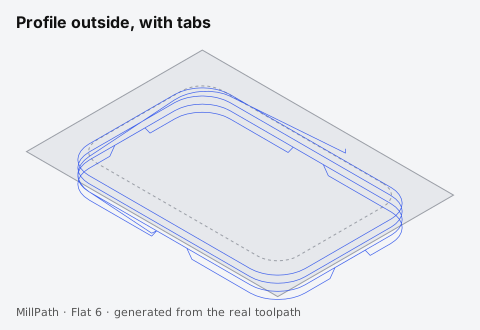
Use it for: Cutting parts out of a sheet, cutting windows and holes larger than the tool, trimming edges.
Tool: A flat end mill (downcut or compression for clean plywood edges).
Settings
| Setting | What it does | Default |
|---|---|---|
| Side | Auto picks outside for an outer outline and inside for a hole; Out, In, or On the line. | Auto |
| Depth | Full depth of the cut. For a cut-out it goes a little below the stock (0.4 mm) to cut cleanly through. | stock thickness + 0.4 mm |
| Stepdown | How deep each pass goes (stepdown). | 2 mm or the tool's own |
| Direction | Climb or conventional milling. | Climb |
| Stock to leave | Material left on the wall for a finishing pass. | 0 |
| Finish passes | Passes that remove the stock to leave in equal steps, at full depth or in levels (Finish stepdown). | 0 |
| Finish stepdown | Finishes a tall wall in levels from the top, each this deep, so a long tool bends less. 0 = the full depth in one pass. | 0 |
| Trochoidal | Cuts a channel a little wider than the tool on the waste side with small loops stepping along it, so the tool takes only a small arc and can go to full depth in one level. The helix starts at the feed height above the stock, and the feed you set is written as it is (corner and arc slowdowns leave it). Not with tabs. | Off |
| Channel width | Width of the channel the loops cut. | 1.4 × tool diameter |
| Step per loop | How far each loop moves along, in % of the tool diameter. | 12 % |
| Finish the wall | Trochoidal: one pass along the wall after the channel (or the finish passes, with stock to leave). Off: the channel only. | On |
| Raise the feed on the loops | Trochoidal: raises the feed on the loops for chip thinning (at most 1.5 ×). | Off |
| Add a finishing operation | One click adds a second profile after this one, on the same shapes and tool, that takes the wall to size in one pass (or in the levels of the finish stepdown). This profile then leaves 0.2 mm on the wall for it (or its own stock to leave), and a trochoidal one cuts the channel only. | |
| Entry | Ramp (slopes down along the cut) or plunge with an arc lead-in. | Ramp |
| Corners | Round (no relief), dogbone or T-bone relief for square inside corners. | Round |
| Tabs | Hold a part in place: number, width and height; placed evenly or by hand on the drawing. | Off |
| Onion skin | Through cuts stop this much above full depth; one last pass per part cuts the skin at the end (vacuum tables). 0 = off. | 0 |
Every operation also has: Tool, Include in G-code, Own safe heights, Start depth, Coolant, see Heights. Hover the (i) next to a setting in the app for the same explanations.
Tips
- Round inside curves (a concave fillet, the inside of a circle) the feed is lowered by centre radius / (centre radius + tool radius): there the cutting edge outruns the tool centre. Into sharp inside corners it drops to 60 % for a tool radius either side.
- With tabs off, parts come loose at the last pass: MillPath warns about it. Use tabs, onion skin, or screws.
- Cut inside features (holes, windows) before the outside profile, so the part is still held.